

Table of Contents
Introduction
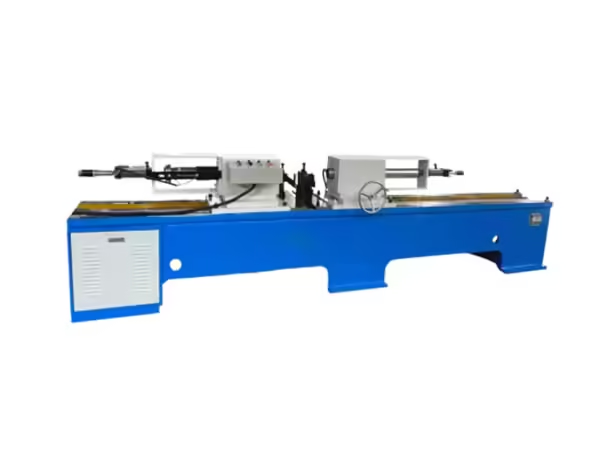
Welding is a critical stage in the manufacture of many conveyor idler rollers because it connects prepared cylindrical components into a stable roller assembly. Before welding begins, the roller tube and related parts have normally passed through cutting, end machining, shaft preparation, and positioning processes. If these earlier stages are inconsistent, maintaining a uniform weld around both ends of the roller becomes more difficult.
A conveyor idler roller welding machine is designed specifically for this repetitive cylindrical welding task. Instead of positioning and welding each roller end separately, a double-end configuration can center the workpiece, clamp it securely, rotate it at a controlled speed, and complete corresponding welds at both ends within one coordinated production cycle.
For batch idler manufacturing, the main advantage is not simply faster welding. Stable centering, repeatable rotational movement, controlled shielding conditions, and coordinated PLC logic can reduce unnecessary variation between workpieces. This guide explains how double-end roller welding works and which factors should be controlled when integrating the process into a conveyor idler production line.
What Is a Conveyor Idler Roller Welding Machine?
A conveyor idler roller welding machine is specialized equipment used to perform circumferential welding on cylindrical roller assemblies. Its structure is designed around the geometry of conveyor rollers, so the machine needs to control workpiece centering, clamping, rotation, welding-head position, and the sequence in which the welding operation takes place.
In a double-end roller welding process, automatic centering and pneumatic clamping establish the workpiece position before both ends are welded simultaneously. PLC-based control coordinates the machine sequence so repeated roller assemblies can follow the same general operating logic.
This differs from a general-purpose welding station. The conveyor roller has a long cylindrical structure and corresponding welding areas at opposite ends, which makes simultaneous double-end processing particularly suitable for batch production.
Why Conveyor Idler Rollers Need Controlled Welding
A conveyor idler roller needs to rotate around a defined central axis. The welded components at both ends therefore need to maintain a consistent relationship with the roller tube and other assembly elements.
If one end is positioned differently from the other, the resulting assembly may no longer reproduce the geometry established during previous machining operations. Welding distortion, inconsistent joint position, or poor centering can also make downstream inspection more difficult.
A conveyor idler roller welding machine creates a controlled mechanical reference before the arc is established. By positioning the workpiece relative to a common machine centerline, manufacturers can reduce the amount of repeated manual alignment required for every roller.
This is especially useful where large batches contain rollers of the same or similar dimensions.
How Double-End Roller Welding Works
The process begins when the prepared roller assembly is loaded into the machine. The workpiece is positioned between the machine supports and aligned with the required working center.
Automatic centering then establishes the relationship between the roller axis and the rotational mechanism. Pneumatic clamping holds the workpiece securely so that its position remains stable when rotation and welding begin.
The welding heads are positioned at the required joints on both ends. Once the welding cycle starts, the roller rotates at a controlled speed while both welding positions operate simultaneously. After the circumferential weld is completed, rotation stops and the machine returns to its initial position.
| Welding Stage | Machine Function | Main Purpose |
|---|---|---|
| Loading | Roller enters machine | Prepare workpiece |
| Centering | Align roller axis | Establish rotation reference |
| Clamping | Stabilize the roller | Prevent unwanted movement |
| Head positioning | Set welding locations | Align with both joints |
| Rotation | Turn cylindrical workpiece | Create circumferential path |
| Double-end welding | Weld both sides | Process corresponding joints |
| Return | Reset machine | Prepare unloading |
| Inspection | Check finished weld | Confirm process consistency |
The quality of the result depends on the stability of the complete sequence rather than on one single machine function.
Why Simultaneous Double-End Welding Is Useful
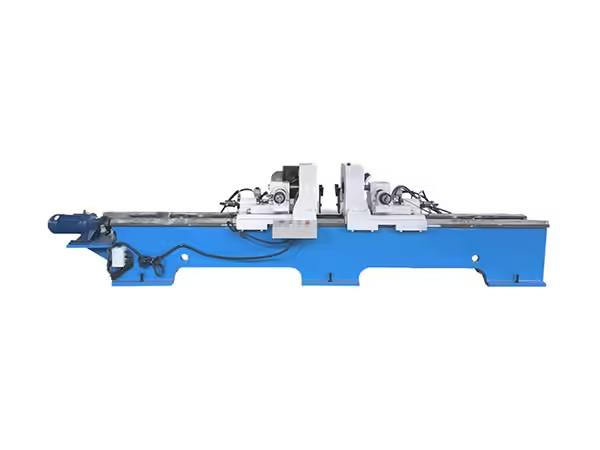
Conveyor idler rollers frequently contain similar welded areas at both ends. If those areas are processed separately, the workpiece needs an additional setup between operations.
Each new setup requires the roller to be repositioned relative to the welding equipment. For long cylindrical components, this can introduce avoidable variation and additional handling.
A conveyor idler roller welding machine with two welding positions keeps both ends referenced within the same machine structure. Once the roller has been centered and clamped, both joints can be processed during the same cycle.
This approach is particularly suitable for repeated production because the relationship between the two ends does not need to be recreated independently for every workpiece.
Automatic Centering and Roller Alignment
Centering is one of the most important stages before welding begins. The roller needs to rotate around an axis that remains predictable relative to the welding heads.
If the workpiece is significantly off-center, the distance between the joint and the welding position can change as the roller rotates. Even when welding parameters remain unchanged, the physical relationship between the torch and the workpiece becomes less stable.
Automatic centering reduces the amount of manual adjustment required before every welding cycle. It helps establish a repeatable mechanical position for cylindrical roller assemblies before clamping and rotation.
However, centering cannot correct badly prepared components. The roller tube, bearing-related parts, and other welded elements still need to arrive at the machine with appropriate geometry.
Gas-Shielded Arc Welding in Roller Production
The equipment uses gas-shielded welding methods suited to steel roller assemblies. Gas metal arc welding uses a continuously fed consumable wire electrode together with shielding gas to protect the weld area from atmospheric contamination. The process can be operated in semi-automatic or automatic systems, which makes it suitable for mechanized roller welding. Wikipedia’s overview of gas metal arc welding explains the underlying wire-electrode and shielding-gas principle.
For conveyor rollers, mechanizing the process allows wire feeding, workpiece rotation, welding position, and machine sequencing to be coordinated more consistently than when every movement is controlled manually.
The actual shielding-gas arrangement and welding parameters should always correspond to the material, wire, joint geometry, and established welding procedure.
Welding Workpiece Diameter and Length
Machine working range needs to match the roller dimensions that will actually be processed.
The TH-220×2200 configuration currently listed on the website supports welding workpiece diameters from Φ76 to Φ219 mm and workpiece lengths from 200 to 2200 mm. These limits affect workpiece support, center position, welding-head adjustment, and the spacing between machine elements.
When production changes between roller specifications, the machine should be adjusted according to the new diameter and length before continuous processing begins.
The first workpiece after a specification change should receive additional inspection so operators can confirm that centering, support, head position, and rotational conditions remain suitable.
Controlled Roller Rotation
Circumferential welding depends on predictable rotational movement. Rather than moving the welding equipment around the entire workpiece, the cylindrical roller can rotate while the welding heads remain at defined positions.
For the TH-220×2200 configuration, the listed welding rotation range is 0–10 rpm/min. The selected rotational condition should correspond to the established welding parameters and the geometry of the joint.
Stable rotation helps maintain a consistent relationship between welding travel and the circumference of the roller.
If rotational speed changes irregularly during the cycle, weld conditions can also change. Drive-system condition and workpiece centering should therefore be included in routine machine inspection.
Why Pneumatic Clamping Matters
Once the roller has been centered, it needs to remain stable throughout the welding cycle.
Pneumatic clamping provides a repeatable method for securing the workpiece before rotation and welding begin. The clamp should hold the roller in the required position without interfering with the rotational system or creating unnecessary deformation.
For batch production, repeatable clamping helps ensure that each roller begins the welding operation from a similar mechanical condition.
Clamping elements also need regular inspection. Wear, contamination, or incorrect adjustment can gradually alter workpiece position even when the PLC program and welding parameters remain unchanged.
PLC Control in an Idler Roller Welding Machine
The welding process requires several actions to happen in the correct order. Centering and clamping should be completed before rotation begins, while welding should only start after the workpiece has reached the required condition.
PLC control coordinates these steps within a defined machine sequence.
This is useful in repeated production because operators do not need to reproduce every control action independently for each roller. Once the mechanical setup and welding parameters have been established, the machine can follow the same operating logic through successive cycles.
PLC control does not replace process inspection. It repeats the programmed sequence, so mechanical alignment, tooling, wire feeding, gas delivery, and component geometry must still remain under control.
Welding Current and Process Stability
Welding current forms part of the established welding procedure and needs to correspond to the workpiece material, joint structure, wire, shielding method, and rotation condition.
The TH-220×2200 specification lists a welding current range of 60–350 A. This describes the available equipment range rather than a universal setting for every roller.
Manufacturers should determine appropriate operating parameters according to the actual roller structure being produced.
Once those parameters have been validated, automatic operation helps reproduce the mechanical sequence surrounding them. Consistency depends on maintaining both the electrical welding conditions and the physical relationship between the roller and welding heads.
Shielding Gas Flow During Welding
Shielding gas protects the weld area while the arc and molten metal are exposed to the surrounding atmosphere.
The current equipment specification lists a shielding-gas flow range of 10–25 L/min. Actual operating conditions should be established according to the welding process, joint, consumable, and surrounding environment.
Gas delivery should remain stable during the welding cycle. Restrictions, leaks, or inconsistent delivery can change shielding conditions even when other machine settings remain unchanged.
For this reason, gas lines, connections, regulators, and associated equipment should form part of routine process inspection.
Upstream Machining Directly Affects Welding
A conveyor idler roller welding machine works most consistently when the incoming components have already been machined accurately.
Tube length and end geometry influence where the welded components sit relative to the roller shell. Shaft and bearing-related assembly processes also affect the final position of the workpiece before it reaches the welding station.
If one component varies significantly, the welding joint may appear in a different position even though the welding machine uses identical settings.
The welding stage therefore needs to be connected with tube processing, shaft machining, bearing setting, and related roller manufacturing operations rather than treated as an isolated process.
Why Welding Should Not Compensate for Poor Assembly
When joint position differs from one roller to another, increasing welding time or changing machine parameters may appear to solve the immediate problem. However, the real cause may be located earlier in production.
Incorrect tube dimensions, poor component positioning, or inconsistent bearing-housing preparation can all alter the geometry presented to the welding machine.
The welding process should therefore join correctly prepared components rather than compensate for dimensional problems created upstream.
A useful troubleshooting principle is to verify workpiece geometry first, then check centering, clamping, rotation, welding-head position, gas delivery, wire feeding, and electrical parameters.
Integrating Welding Into Conveyor Roller Production
Roller welding is only one stage in a larger manufacturing sequence.
A typical process can include tube cutting, tube-end machining, shaft preparation, component assembly, bearing setting, welding, and final inspection. The exact order depends on the roller design and manufacturing method.
Each operation should prepare the workpiece for the stage that follows. If tube machining produces inconsistent components, assembly and welding become harder to control. If pressing introduces positioning variation, the welding joint may no longer appear at the intended location.
A well-organized production line therefore treats the conveyor idler roller welding machine as one coordinated part of the complete roller manufacturing system.
Balancing Welding Capacity With Other Machines
A welding machine may be capable of completing a cycle quickly, but overall production output depends on the surrounding processes.
If tube-end machining or bearing assembly supplies workpieces more slowly than welding can process them, the welding station will spend part of its time waiting. If inspection or another downstream stage is slower, completed rollers may accumulate after welding.
Manufacturers should therefore compare cycle times across the production line instead of evaluating welding equipment only by its individual operating speed.
Balanced capacity helps reduce excessive work-in-process material and provides a clearer path for future production expansion.
Changing Between Roller Specifications
Factories often manufacture several roller diameters and lengths. A conveyor idler roller welding machine therefore needs a practical setup method for moving between product specifications within its designed working range.
Changes can affect support position, welding-head location, workpiece centering, clamping, and rotational settings.
Validated setups for frequently produced rollers can help reduce repeated trial adjustment. Recording appropriate machine positions and process parameters gives operators a clearer starting point when a specification returns to production.
After every significant setup change, the first finished roller should be inspected carefully before a larger batch proceeds.
Common Causes of Welding Variation
Inconsistent roller welding can originate from several sources.
Workpieces may not be centered correctly, clamping can become unstable, or incoming components may vary dimensionally. Welding-head position can also change if machine adjustments are not maintained.
Wire feeding, shielding gas delivery, rotational movement, and established electrical parameters should also be checked.
Instead of changing several settings at once, troubleshooting should follow the production sequence. Confirm the workpiece first, then verify centering, clamping, rotation, welding-head position, wire feeding, shielding conditions, and machine control.
This approach helps identify where variation actually begins.
Inspecting the Finished Roller Weld
Inspection after welding should confirm that the joint has been completed according to the manufacturing requirements before the roller proceeds further.
Visual checks can identify obvious discontinuities, irregular surface conditions, inconsistent joint position, or differences between the two ends.
Because the machine processes both ends simultaneously, comparing the left and right welds can provide useful information about setup consistency.
Manufacturers may also perform additional dimensional or functional checks according to the roller design and internal quality-control requirements.
Inspection data should be used as feedback for production, not only as a method of separating acceptable and unacceptable workpieces.
Maintaining Welding Heads and Wire Feeding
Reliable automated welding requires stable delivery of welding wire and correct positioning of the welding heads.
Wire-feeding components should operate smoothly and remain free from conditions that cause irregular feed movement. Consumable parts should also be inspected according to the welding procedure and equipment requirements.
The welding heads need to maintain the intended position relative to the rotating workpiece. Mechanical looseness or incorrect adjustment can change the joint relationship even when other settings remain identical.
Routine inspection of these systems supports more stable batch production.
Maintaining the Rotation and Clamping Systems
The rotation and clamping mechanisms are equally important because they control how the roller behaves mechanically during welding.
Drive components should maintain predictable rotational movement, while pneumatic elements should continue to position the workpiece securely.
Material debris and welding contamination should be removed from areas where they can affect supports, clamps, or moving mechanisms.
Changes in machine sound, rotational behavior, clamping movement, or workpiece stability should be investigated before they begin to affect repeated welding results.
Maintenance therefore contributes directly to welding-process consistency.
When a Conveyor Idler Roller Welding Machine Is Most Useful
This type of equipment is particularly suitable for manufacturers producing repeated batches of cylindrical rollers with corresponding welded areas at both ends.
The double-end structure takes advantage of the roller’s symmetrical geometry, while automatic centering and controlled rotation reduce repeated manual setup.
The machine is especially useful when upstream production already supplies dimensionally consistent components because stable incoming parts allow the automated welding cycle to operate under more predictable conditions.
Manufacturers processing many different roller sizes can also benefit from an adjustable machine structure, provided the products remain within the designed diameter and length range.
How to Evaluate a Conveyor Idler Roller Welding Machine
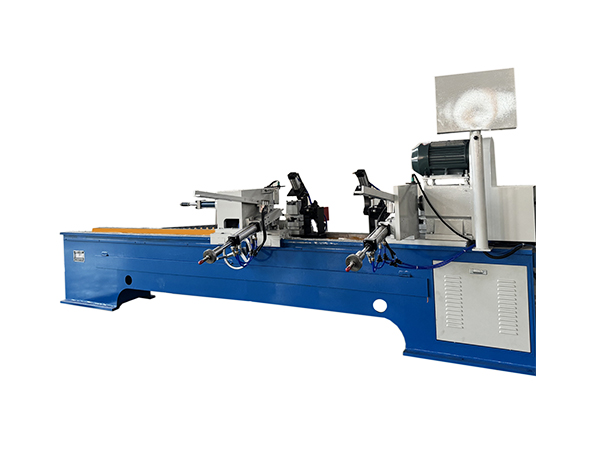
Machine evaluation should begin with the roller drawing and actual welding process.
Manufacturers should identify workpiece diameter, length, joint location, material, required welding process, rotational conditions, shielding method, and the production stages immediately before and after welding.
The machine’s centering method, clamping system, working range, rotational control, welding-current range, PLC system, head adjustment, and maintenance requirements can then be compared with those manufacturing needs.
The objective should be to select equipment that fits the entire production sequence rather than simply maximizing one isolated welding parameter.
Conclusion
A conveyor idler roller welding machine provides a controlled method for completing circumferential welding during conveyor roller production. By combining automatic centering, pneumatic clamping, controlled rotation, double-end simultaneous welding, and PLC-based sequencing, the equipment can reduce repeated manual positioning and create a more consistent production cycle.
Stable welding still depends on correctly prepared components, suitable welding parameters, shielding-gas delivery, workpiece alignment, wire feeding, machine condition, and inspection. Automation works best when these factors are already organized into a defined manufacturing process.
When welding is coordinated with tube processing, shaft machining, bearing assembly, and downstream inspection, it becomes a predictable stage within the complete conveyor idler manufacturing workflow rather than an isolated operation.
FAQ
What is a conveyor idler roller welding machine used for?
A conveyor idler roller welding machine performs controlled circumferential welding on roller assemblies. It centers and clamps the cylindrical workpiece, controls rotation, and can weld corresponding joints at both ends during one coordinated cycle, making it suitable for repeated idler production.
Why is double-end welding suitable for conveyor idler rollers?
Idler rollers often contain similar welded joints at opposite ends. Double-end equipment processes both sides while the roller remains in one machine setup, reducing repeated repositioning and helping maintain a more consistent relationship between corresponding joints throughout batch manufacturing.
What workpiece sizes can the TH-220×2200 process?
The listed TH-220×2200 configuration supports workpiece diameters from Φ76 to Φ219 mm and lengths from 200 to 2200 mm. Setup must also consider joint position, workpiece support, clamping, welding-head location, rotation settings, and the geometry of incoming components.
Why is automatic centering important during roller welding?
Automatic centering aligns the cylindrical roller with the rotational system before welding begins. A stable centerline helps keep the joint in a predictable relationship with the welding heads as the workpiece rotates, reducing the amount of repeated manual alignment required between rollers.
What should be checked after automatic roller welding?
Inspection should examine joint position, visible weld continuity, surface condition, symmetry between both ends, and overall workpiece condition according to the roller design. Repeated differences can indicate issues with centering, clamping, rotation, welding-head position, or upstream component dimensions.



 English
 French
 Spanish