

Table of Contents
Introduction

Steel pipe preparation is one of the earliest manufacturing stages in conveyor roller production. Before a tube can enter double-end machining, bearing housing assembly, welding, and inspection, the raw pipe must first be divided into blanks with controlled length and suitable end-face quality. Variation created during this stage can continue into every process that follows.
A cold cutting pipe machine provides a mechanical approach to this operation. Instead of using a flame, laser beam, or plasma arc to separate the material, the steel pipe is cut through controlled mechanical tool movement. In the pipe cutting equipment used for conveyor roller production, the long workpiece remains stationary while the cutting tool rotates around it.
This structure is particularly suitable for repeated straight cutting of round steel pipe. Servo feeding controls the required blank length, hydraulic clamping stabilizes the workpiece, and PLC-based sequencing coordinates the cutting cycle. The result is a process designed around repeatable roller shell preparation rather than complex profile cutting.
What Is a Cold Cutting Pipe Machine?
In this context, a cold cutting pipe machine refers to equipment that separates steel pipe through mechanical cutting rather than a thermal cutting process.
The automatic steel pipe cutting equipment used for roller manufacturing automatically completes feeding, positioning, clamping, and cutting. Its operating principle keeps the workpiece stationary while the cutter holder rotates.
This distinction is important because different pipe-cutting technologies are designed for different tasks. Thermal equipment may be useful where complex contours or profiles are required, while mechanical cutting can be highly suitable when manufacturers repeatedly need straight cylindrical blanks.
Conveyor roller production normally requires the latter. Raw round steel pipe needs to be divided into consistent sections that can proceed directly into tube-end processing.
Why Mechanical Cold Cutting Fits Conveyor Roller Production
A conveyor roller shell is normally a straight cylindrical component. It does not usually require a complex saddle cut, branch opening, or three-dimensional profile before entering the next manufacturing stage.
The primary cutting requirements are therefore comparatively focused:
- consistent finished length;
- controlled end-face geometry;
- manageable burr formation;
- stable repeatability;
- suitable preparation for later machining.
A cold cutting pipe machine can concentrate on these requirements without introducing a thermal process that is unnecessary for the basic straight-cut operation.
The mechanical cutting approach also creates a predictable link between tube feeding distance and finished blank length, which is particularly useful when identical roller shells are produced repeatedly.
How the Cold Cutting Process Works
The process begins when a long steel pipe is placed into the feeding system. The pipe passes through the machine spindle and is advanced according to the required cutting length.
Once the programmed position has been reached, the clamping system secures the workpiece.
The pipe itself does not rotate. Instead, the cutter holder rotates around the stationary tube and progressively removes material until the section is separated.
After cutting, the tool retracts, the clamping system releases the workpiece, and the servo feeding mechanism advances the material for the next cycle.
| Production Stage | Machine Action | Main Purpose |
|---|---|---|
| Material feeding | Servo advances steel pipe | Establish blank length |
| Positioning | Pipe stops at programmed point | Control cutting location |
| Hydraulic clamping | Secures round steel pipe | Stabilize workpiece |
| Cutter rotation | Tool moves around stationary pipe | Separate material |
| Tool retraction | Cutter returns | Complete cutting cycle |
| Material advance | Servo feeds next section | Prepare repeated cut |
| Inspection | Check finished blank | Protect downstream quality |
The quality of the finished blank depends on all these stages working together.
Why the Steel Pipe Remains Stationary
One of the key structural characteristics of the machine is that the steel pipe remains stationary during cutting.
This is especially useful when processing long raw tubes.
If a long pipe needed to rotate at cutting speed, manufacturers would need to manage its balance, support, alignment, and surrounding clearance throughout the rotation. Longer stock can make this increasingly difficult.
Keeping the workpiece stationary avoids this issue.
The tube moves only in the longitudinal feeding direction. Once it reaches the correct position, hydraulic clamping holds it while the cutter holder performs the rotational movement.
For roller manufacturing, this arrangement creates a practical way to process long stock while maintaining a stable relationship between the pipe, feeding mechanism, clamps, and cutting point.
Servo Feeding Controls the Finished Length
The cutting tool cannot create a consistent roller blank if the pipe arrives at a different position during every cycle.
This is why feeding accuracy is one of the most important parts of a cold cutting pipe machine.
The current Pipe Cutting Machine uses a servo motor together with a ball screw for material feeding. The control system determines how far the raw pipe advances before the next cutting operation begins.
Because the movement follows a defined position command, manufacturers can reduce dependence on repeated manual measurement.
When a production specification changes, the required cutting length can be adjusted according to the new roller shell dimensions.
The first completed workpiece should still be measured carefully to confirm the setup before a longer batch proceeds.
Hydraulic Self-Centering Clamping
After feeding, the workpiece must remain stable during the cutting operation.
The QZ160 configuration uses self-centering hydraulic clamping. This is important for round steel pipe because the workpiece needs to remain centered relative to the cutter rotation.
If the tube moves during cutting, end-face condition and dimensional consistency may change even when the servo feeding position was correct.
A stable clamp therefore protects the accuracy established by the feeding system.
Clamping components should also be inspected regularly. Wear, chips, contamination, or incorrect adjustment can gradually alter how the tube sits inside the machine.
Cutting Range for Round Steel Pipe
The QZ160 Pipe Cutting Machine is designed for round steel pipe within a specified working range.
The listed cutting diameter is approximately Φ60–159 mm, with a cutting thickness range of 3–8 mm.
These figures should be considered together rather than independently.
A pipe with a particular outside diameter can behave differently depending on wall thickness, material condition, and tooling. Machine setup therefore needs to correspond with the complete tube specification.
Different machine configurations can also support different production ranges, so manufacturers should match the equipment to the roller families they actually produce.
Cutting Tools and Material Removal
The current equipment can use white steel or carbide cutting tools according to the processing requirement.
Tool material and tool condition influence how the cutting edge interacts with the steel pipe.
As a tool gradually wears, cutting resistance can increase and the finished edge may begin to change. Burr formation, cutting sound, surface appearance, or machine load can provide useful indications that tooling deserves inspection.
Tool management should therefore form part of routine production control.
Replacing a tool only after it has already created a large number of inconsistent blanks makes downstream manufacturing more difficult.
Cold Cutting vs Thermal Pipe Cutting
Industrial pipe cutting can be performed using different technologies depending on material, geometry, and the required finished condition.
Thermal processes rely on concentrated heat to separate material. Mechanical processes remove material through physical cutting-tool contact.
For conveyor roller shells, the workpiece usually requires a straight transverse cut rather than a complex profile.
This makes mechanical cutting particularly relevant because the machine can focus on accurate feeding, secure clamping, tool rotation, and repeatable straight separation.
The selection of cutting technology should therefore begin with the finished part rather than assuming that a more complex cutting process is automatically more suitable.
No Need to Rotate Long Steel Stock
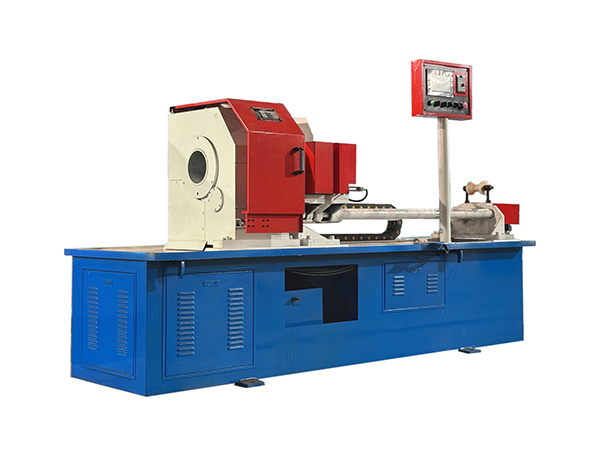
The stationary-pipe configuration provides another manufacturing advantage: the support system does not need to accommodate high-speed rotation of the entire raw tube.
Long material can remain aligned along the machine feeding axis.
Support racks can carry the stock while the servo mechanism controls longitudinal movement. When the correct position is reached, the workpiece is clamped and the cutter rotates locally around the cutting area.
This simplifies the mechanical behavior of long stock and makes the process easier to integrate into continuous roller shell preparation.
End-Face Quality Matters After Cutting
Cutting is not the final machining stage for a conveyor roller shell.
The blank normally proceeds into additional tube-end processing before bearing housings or related components are assembled.
For this reason, the cut face should provide a suitable starting condition for the next machine.
Large angular errors, severe burrs, deformation, or inconsistent blank lengths can create additional work during subsequent processing.
A cold cutting pipe machine should therefore be evaluated according to the quality of the blank it delivers downstream, not simply by whether it successfully separates the steel pipe.
Burr Formation and Tool Condition
Mechanical cutting can create burrs around the separated edge.
The objective is not necessarily to eliminate every microscopic edge condition during the cutting operation, but to keep burr formation predictable and controlled.
Several factors influence the result:
tool sharpness, feed conditions, tube wall thickness, clamping stability, spindle condition, and material characteristics.
If burrs gradually become heavier during a production batch, tooling should be inspected before machine settings are changed unnecessarily.
A worn tool is often easier to correct than allowing inconsistent blanks to continue into the next manufacturing stage.
Connecting Cutting With Double-End Tube Machining
After cutting, the steel tube blank may move into specialized end machining.
The existing roller manufacturing machinery includes an Automatic Roller Double End Holes Lathe designed specifically for machining both ends of steel pipe used in belt conveyor rollers.
This creates a direct relationship between the two manufacturing stages.
The cold cutting pipe machine determines the starting blank length and end-face condition. Double-end machining then establishes the more precise geometry required for later roller components.
If the cutting stage produces consistent blanks, the following machine receives a more predictable starting workpiece.
Why Cutting Length Variation Creates Downstream Problems
Imagine that a production batch contains roller shells whose initial lengths vary significantly.
The double-end machining stage may then need to remove different amounts of material from each workpiece. This makes the process less predictable and can complicate final length control.
Variation can continue further into bearing assembly and welding.
The earliest production stages therefore deserve strong dimensional control because errors introduced there can become embedded in several downstream operations.
A cold cutting pipe machine helps establish one of the first repeatable dimensional references in the roller manufacturing process.
PLC Control and Repetitive Cutting
The machine uses PLC-based control to coordinate the cutting sequence.
The control logic can organize feeding, positioning, clamping, cutting movement, tool return, and the start of the next cycle.
This makes repeated production easier to standardize.
However, PLC control does not eliminate the need for mechanical inspection.
A programmed feed distance can remain identical while a worn ball screw, loose support, damaged tool, or unsuitable clamp introduces physical variation.
Automation provides repeatability only when the mechanical system supporting it remains in controlled condition.
Frequency-Controlled Spindle Speed
The cutter spindle uses frequency-conversion speed regulation.
This allows rotational conditions to be adjusted according to the workpiece and cutting setup rather than relying on only one fixed speed.
The appropriate setting should correspond with pipe diameter, wall thickness, material, and tool condition.
Increasing speed without considering these factors does not automatically create a better cut.
A stable cutting process balances tool rotation, tool feed, workpiece clamping, and material characteristics.
QZ160 Cutting Parameters
The QZ160 model provides a useful example of the machine’s working structure.
| Parameter | QZ160 |
|---|---|
| Pipe diameter | Φ60–159 mm |
| Wall thickness | 3–8 mm |
| Main motor | 5.5 kW |
| Workpiece movement | Stationary during cutting |
| Cutter movement | Rotating |
| Clamping | Self-centering hydraulic |
| Feeding | Servo motor + ball screw |
| Single feed length | 20–1200 mm |
| Tool options | White steel / carbide |
| Feed rate | 0.09/r |
The listed cutting reference for a Φ89 × 2.5 mm tube is approximately 15 seconds. Actual production conditions depend on material, tooling, setup, and workpiece specification.
Machine Selection Should Begin With the Roller Drawing
A cold cutting pipe machine should be selected according to the roller shells that will actually be produced.
Important information includes:
- roller tube outside diameter;
- wall thickness;
- raw material length;
- finished blank length;
- steel specification;
- production batch structure;
- downstream machining process;
- required dimensional consistency.
These factors determine whether the machine working range and feeding structure correspond with the production requirement.
The objective should be to create suitable blanks for the complete manufacturing process rather than optimize an isolated cutting operation.
Handling 6-Meter and Longer Steel Pipe
Industrial roller production commonly begins with long raw steel tube.
The feeding and support system should keep this material aligned as it moves toward the cutting position.
Long stock needs enough support to prevent excessive sagging or side movement. The feeding axis, material rack, and machine spindle should work together to maintain a predictable path.
Improper support can reduce the benefit of an accurate servo system because the workpiece itself may not enter the machine consistently.
Material handling should therefore be included in the cutting process design.
First-Piece Inspection After Changing Length
When the required roller length changes, manufacturers should avoid immediately processing a full batch.
The first cut blank provides an opportunity to verify whether the new servo feeding setting corresponds with the intended finished length.
Useful checks include:
finished length, end-face condition, burr level, visible deformation, and general consistency of the cutting surface.
If the first piece is correct, continuous production can proceed with greater confidence.
Periodic measurements should still be made during the batch to confirm that the process remains stable.
Diagnosing Length Errors
When finished blank length begins to vary, troubleshooting should follow the actual process sequence.
First, check the raw material and material support.
Next, verify servo feeding movement and mechanical transmission. The ball screw, guides, stops, and related positioning components should operate correctly.
The clamping system should then be inspected to confirm the pipe is not moving after it reaches position.
Only after these areas have been checked should operators begin changing control settings.
This structured approach makes it easier to identify the actual source of the dimensional variation.
Diagnosing Poor End-Face Quality
Poor end-face condition can have a different set of causes from incorrect cutting length.
Tool wear is one of the first factors to inspect. The cutter should also be mounted correctly and operate under suitable rotational and feed conditions.
Workpiece clamping should remain stable throughout cutting.
Excessive vibration, worn spindle components, inappropriate tool geometry, or material variation can also influence the finished surface.
Troubleshooting should separate dimensional problems from cutting-surface problems rather than assuming one machine adjustment will solve both.
Why Cold Cutting Supports Later Welding
The cutting operation occurs long before final roller welding, but the two stages are still connected.
Consistent tube blanks make subsequent end machining and component positioning easier to control.
When the prepared roller eventually reaches the welding station, corresponding joints are more likely to appear in predictable positions.
In contrast, large blank variation can force later processes to compensate repeatedly.
This illustrates why manufacturing quality should be understood across the complete roller production sequence.
Cutting for Continuous Roller Manufacturing
The Pipe Cutting Machine is designed around repeated processing rather than occasional manual separation.
Automatic feeding and cutting allow long pipe stock to be divided into multiple roller shell blanks using one established setup.
This is particularly useful when manufacturers produce a batch of rollers sharing the same tube diameter and length.
Once the first piece has been verified, subsequent blanks can follow the same programmed feeding and cutting sequence.
This creates a stable foundation for batch roller manufacturing.
Cold Cutting Pipe Machine vs Manual Cutting
Manual pipe cutting can be appropriate for occasional workshop operations, but repeated roller production has different requirements.
The operator would otherwise need to measure, position, clamp, cut, and remeasure each blank independently.
A cold cutting pipe machine integrates these actions into a controlled cycle.
| Factor | Manual Cutting | Automatic Mechanical Cutting |
|---|---|---|
| Length positioning | Repeated manual measurement | Servo-controlled feeding |
| Clamping | Operator-dependent | Hydraulic self-centering |
| Tool movement | Manual or separate machine | Controlled rotating cutter |
| Repeatability | More dependent on operator | Defined machine sequence |
| Batch production | More handling required | Repetitive cycle |
| Process integration | Limited | Suitable for roller workflow |
The advantage becomes more significant as production becomes repetitive.
Maintenance of the Feeding System
The feeding system directly influences finished length.
Servo motors, ball screws, guides, bearings, and supporting components should remain in suitable condition.
Lubrication, fastening, alignment, and cleanliness all matter because chips or contamination can interfere with smooth movement.
Changes in feeding sound, positioning behavior, or repeatability can provide early warning that inspection is required.
Preventive maintenance is more effective than waiting until dimensional variation becomes obvious across a production batch.
Maintaining the Hydraulic Clamping System
The hydraulic clamping system needs to secure the steel pipe consistently.
Hydraulic pressure, cylinder condition, seals, valves, clamps, and contact surfaces should be inspected according to machine requirements.
A slow leak or worn clamping surface can gradually reduce workpiece stability.
Because the pipe remains stationary during cutting, secure clamping is fundamental to the machine’s operating principle.
Maintenance of the clamping system therefore directly supports cutting consistency.
Cutter and Spindle Maintenance
The rotating cutter holder and spindle perform the primary material-removal operation.
Tool holders should remain secure, while the spindle needs stable rotation without abnormal vibration or looseness.
Cutting tools should be inspected according to their actual workpiece results rather than only by elapsed operating time.
Changes in burr formation, cutting sound, end-face condition, or machine load can all provide useful maintenance signals.
Keeping this system in controlled condition helps protect both cutting quality and downstream machining consistency.
Where a Cold Cutting Pipe Machine Fits in Roller Production
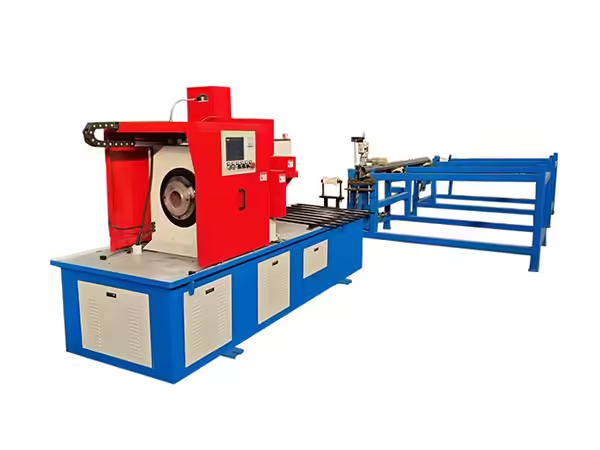
The machine is positioned near the beginning of the manufacturing sequence.
A typical workflow can include:
steel tube preparation → mechanical pipe cutting → double-end tube machining → component preparation → bearing assembly → roller welding → final inspection.
The exact production route depends on the roller design.
The cutting machine’s responsibility is to provide predictable tube blanks to the following operation.
When this first dimensional stage is controlled effectively, the remaining roller manufacturing processes begin from a more consistent foundation.
Conclusion
A cold cutting pipe machine provides a practical mechanical method for preparing round steel pipe used in conveyor roller manufacturing. By keeping the workpiece stationary while the cutter rotates, the machine avoids the need to rotate long steel stock during the cutting operation.
Servo feeding establishes the blank length, hydraulic self-centering clamping stabilizes the pipe, and PLC control coordinates the repetitive production sequence. Mechanical cutting also provides a suitable approach for straight roller shell preparation without relying on laser, plasma, or flame-based processes.
Reliable performance still depends on raw material quality, support alignment, servo feeding accuracy, hydraulic clamping, tool condition, spindle stability, first-piece inspection, and preventive maintenance.
When the cutting process delivers consistent blanks, double-end tube machining, bearing assembly, welding, and final inspection can operate from a more predictable starting condition. This makes mechanical pipe cutting an important early stage in a controlled conveyor roller manufacturing workflow.
FAQ
What is a cold cutting pipe machine used for?
A cold cutting pipe machine mechanically separates round steel pipe into controlled sections without using a laser, plasma arc, or flame-based cutting process. In conveyor roller manufacturing, it prepares steel tube blanks that later enter tube-end machining, assembly, welding, and inspection.
How does the steel pipe remain stable during cold cutting?
The pipe is advanced to the required position through servo-controlled feeding and then secured by a self-centering hydraulic clamping system. During cutting, the workpiece remains stationary while the cutter holder rotates, maintaining a stable relationship between the tube, clamp, and cutting point.
What pipe range can the QZ160 machine process?
The QZ160 configuration is specified for round steel pipe diameters of approximately Φ60–159 mm and wall thicknesses of 3–8 mm. Its feeding system uses a servo motor and ball screw, while single feeding length is listed at approximately 20–1200 mm for repetitive blank preparation.
Why is cold cutting suitable for conveyor roller shells?
Roller shells normally require repeated straight transverse cuts rather than complex pipe profiles. Mechanical cutting can focus on blank length, end-face condition, burr control, and repeatability while keeping long stock stationary, creating a suitable starting workpiece for later double-end tube machining.
What should be inspected after mechanical pipe cutting?
Finished blanks should be checked for length, end-face condition, burr formation, visible deformation, and consistency between repeated pieces. The first blank after a specification change deserves additional inspection, while periodic measurements during batch production help identify gradual changes in tooling or feeding accuracy.


 English
 French
 Spanish